 Djinious




Bellini Foods — Aseptic Bottling Line 3
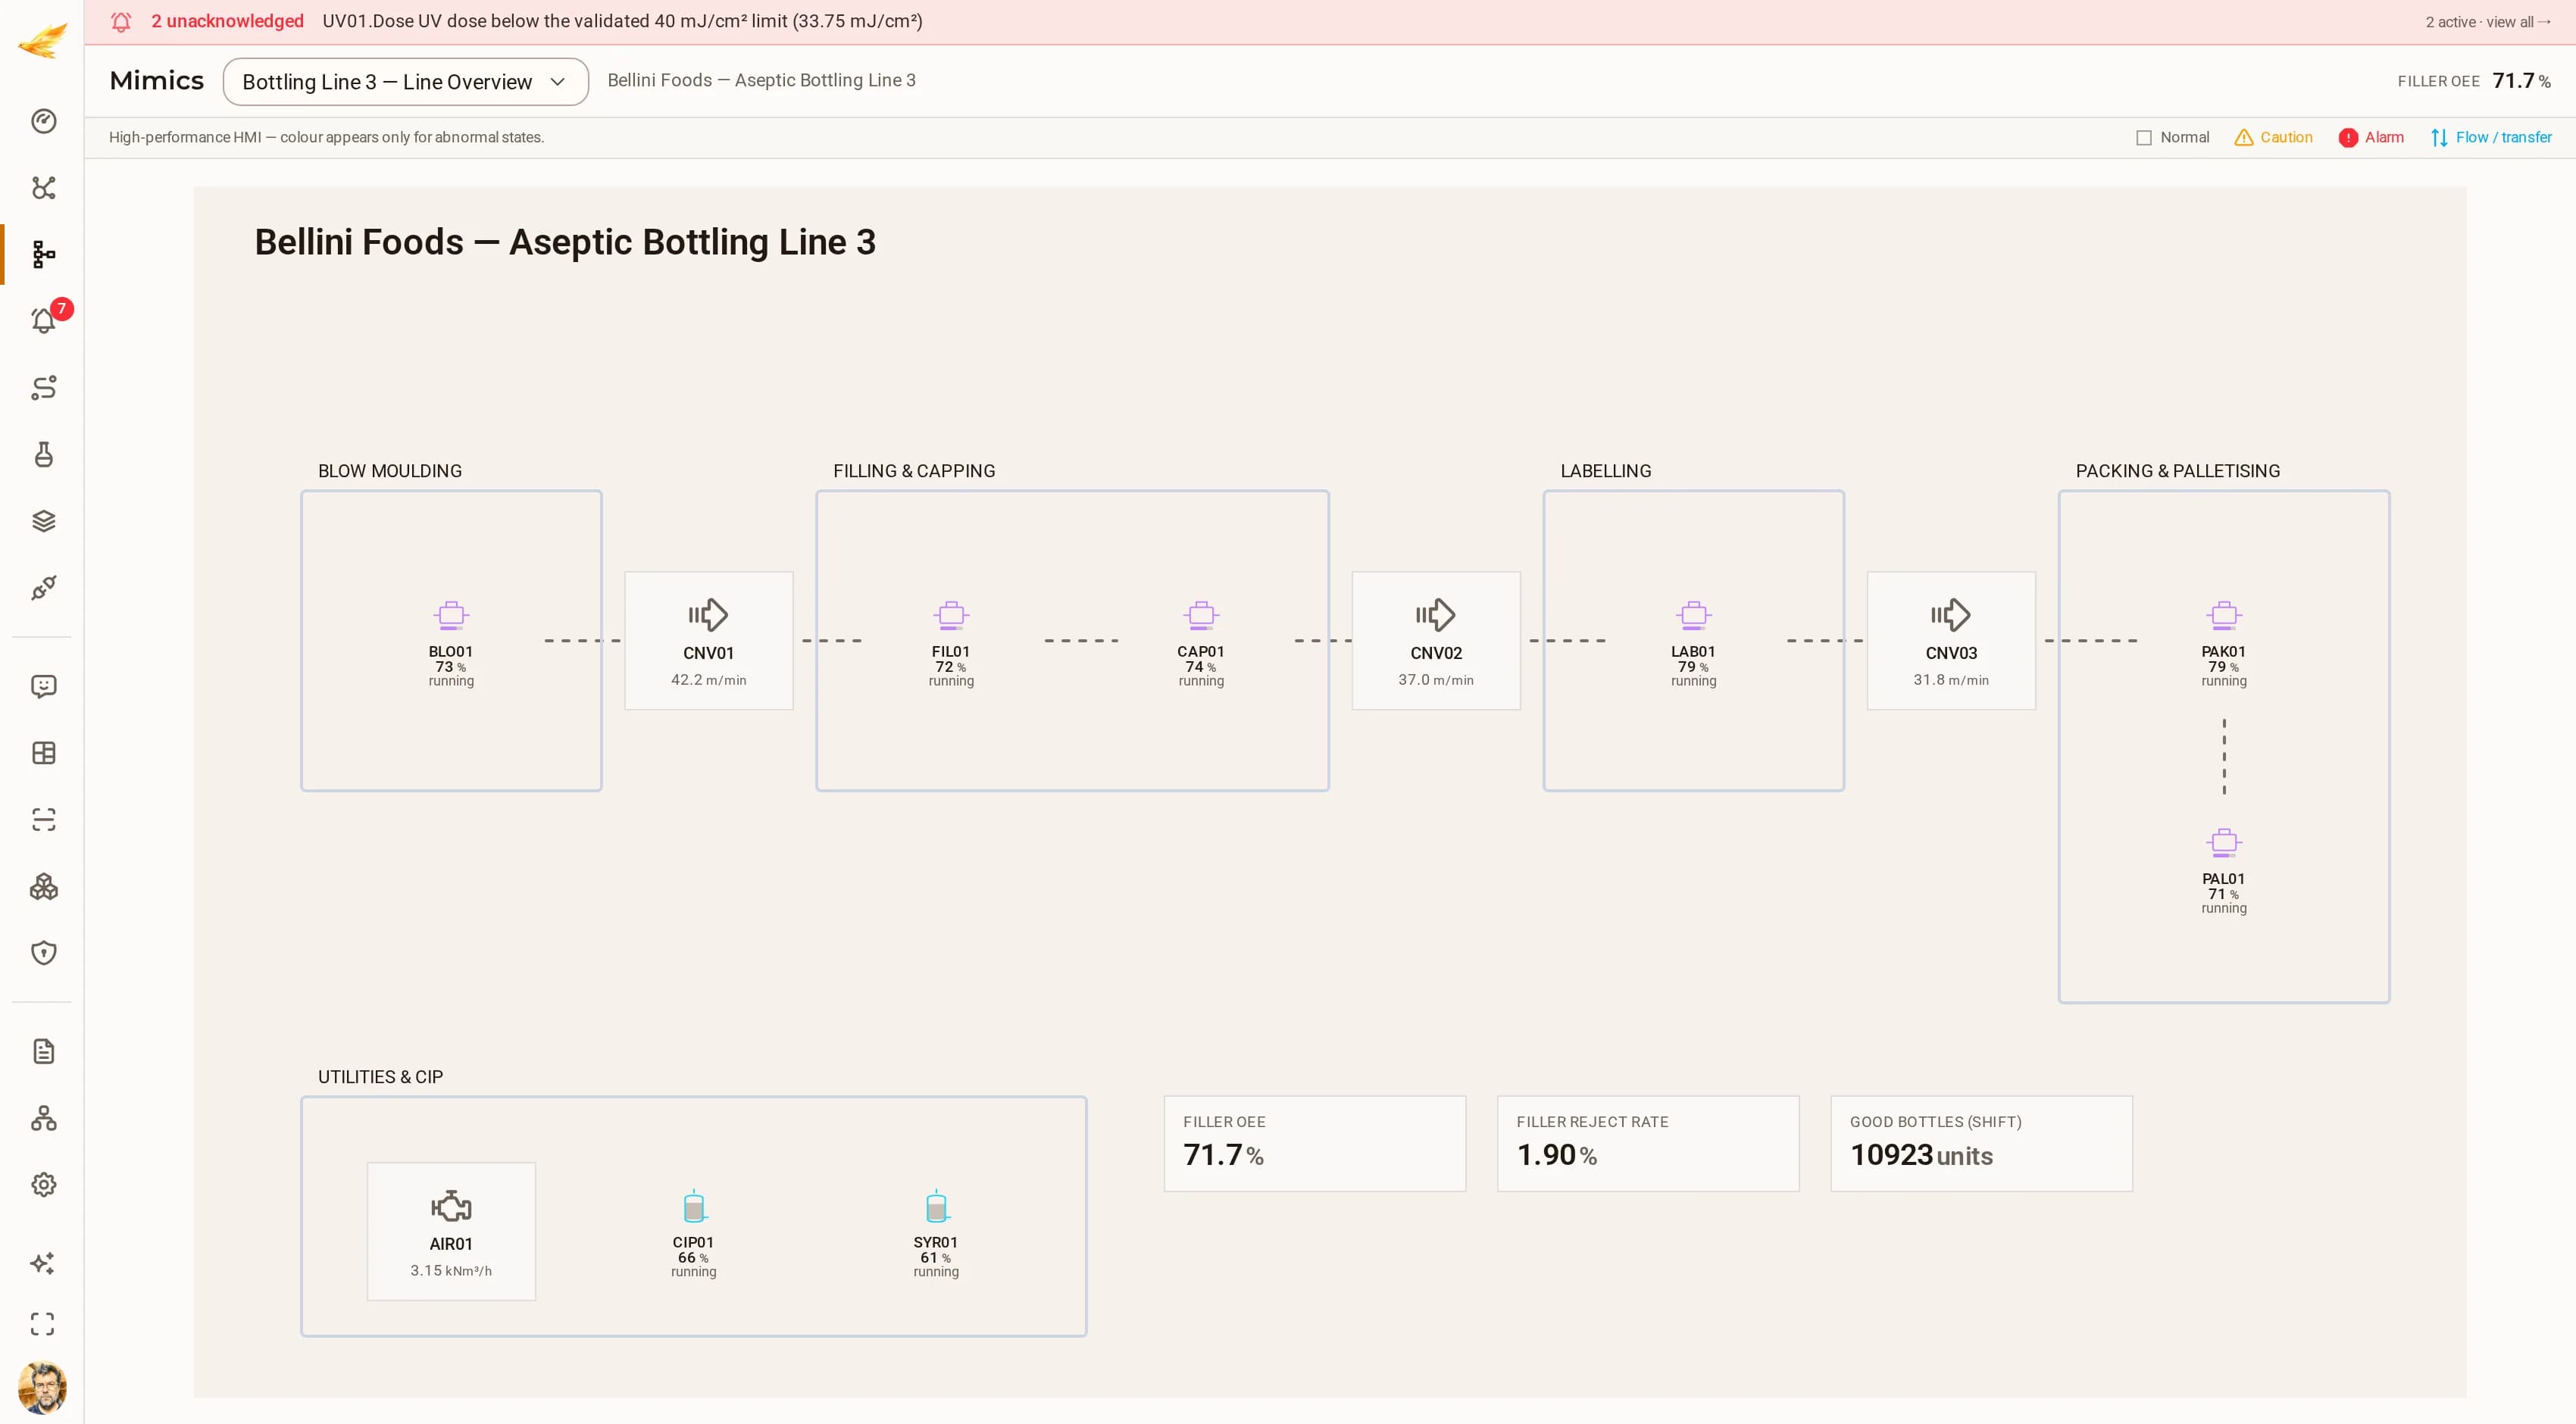
A 24 000 bottles/hour aseptic PET line: blow moulding, aseptic filling, capping, labelling, case packing and palletising, with live OEE on every machine and its own utilities and CIP block.
 DjiniousCC
- site code
- BLN3site code
- assets
- 12assets
- live tags
- 95live tags
- authority class
- C4authority classoperational action
Site BLN3, Parma, Italy. These are not mock-ups: all five sites run side by side in the same DjiniousCC instance — 99 assets and 693 live tags, acquired at 1 Hz, historised, alarmed, and each with a procedure that has been dry-run and proven on an isolated twin.
Chasing output past the quality knee costs more than it makes
Push the line to 100 % of the filler's nameplate rate and fill-level and seal rejects climb past 9 %. The extra bottles produced never cover the bottles scrapped, and on an aseptic line a reject excursion is a food-safety review, not just a yield number.
What the platform models here
Each family has a behavioural model that the live simulator and the proving twin share, so a dry-run behaves the way the plant does.
Blow moulder · Aseptic filler · Capper · Labeller · Case packer · Palletiser · Accumulation conveyors · Plant air · CIP & syrup tanks
The procedure: Line 3 Overspeed Reject Recovery
Bring the aseptic filler back inside its quality window after an overspeed push: trim the filler and the machines either side of it back to the balanced line rate, and require line-supervisor confirmation before the change is applied. Authority class: C4 · operational action.
Step 1
Trim filler → 86 %
Step 2
Trim capper → 86 %
Step 3
Trim labeller → 86 %
Step 4
Line-supervisor confirmation
Step 5
Notify line office
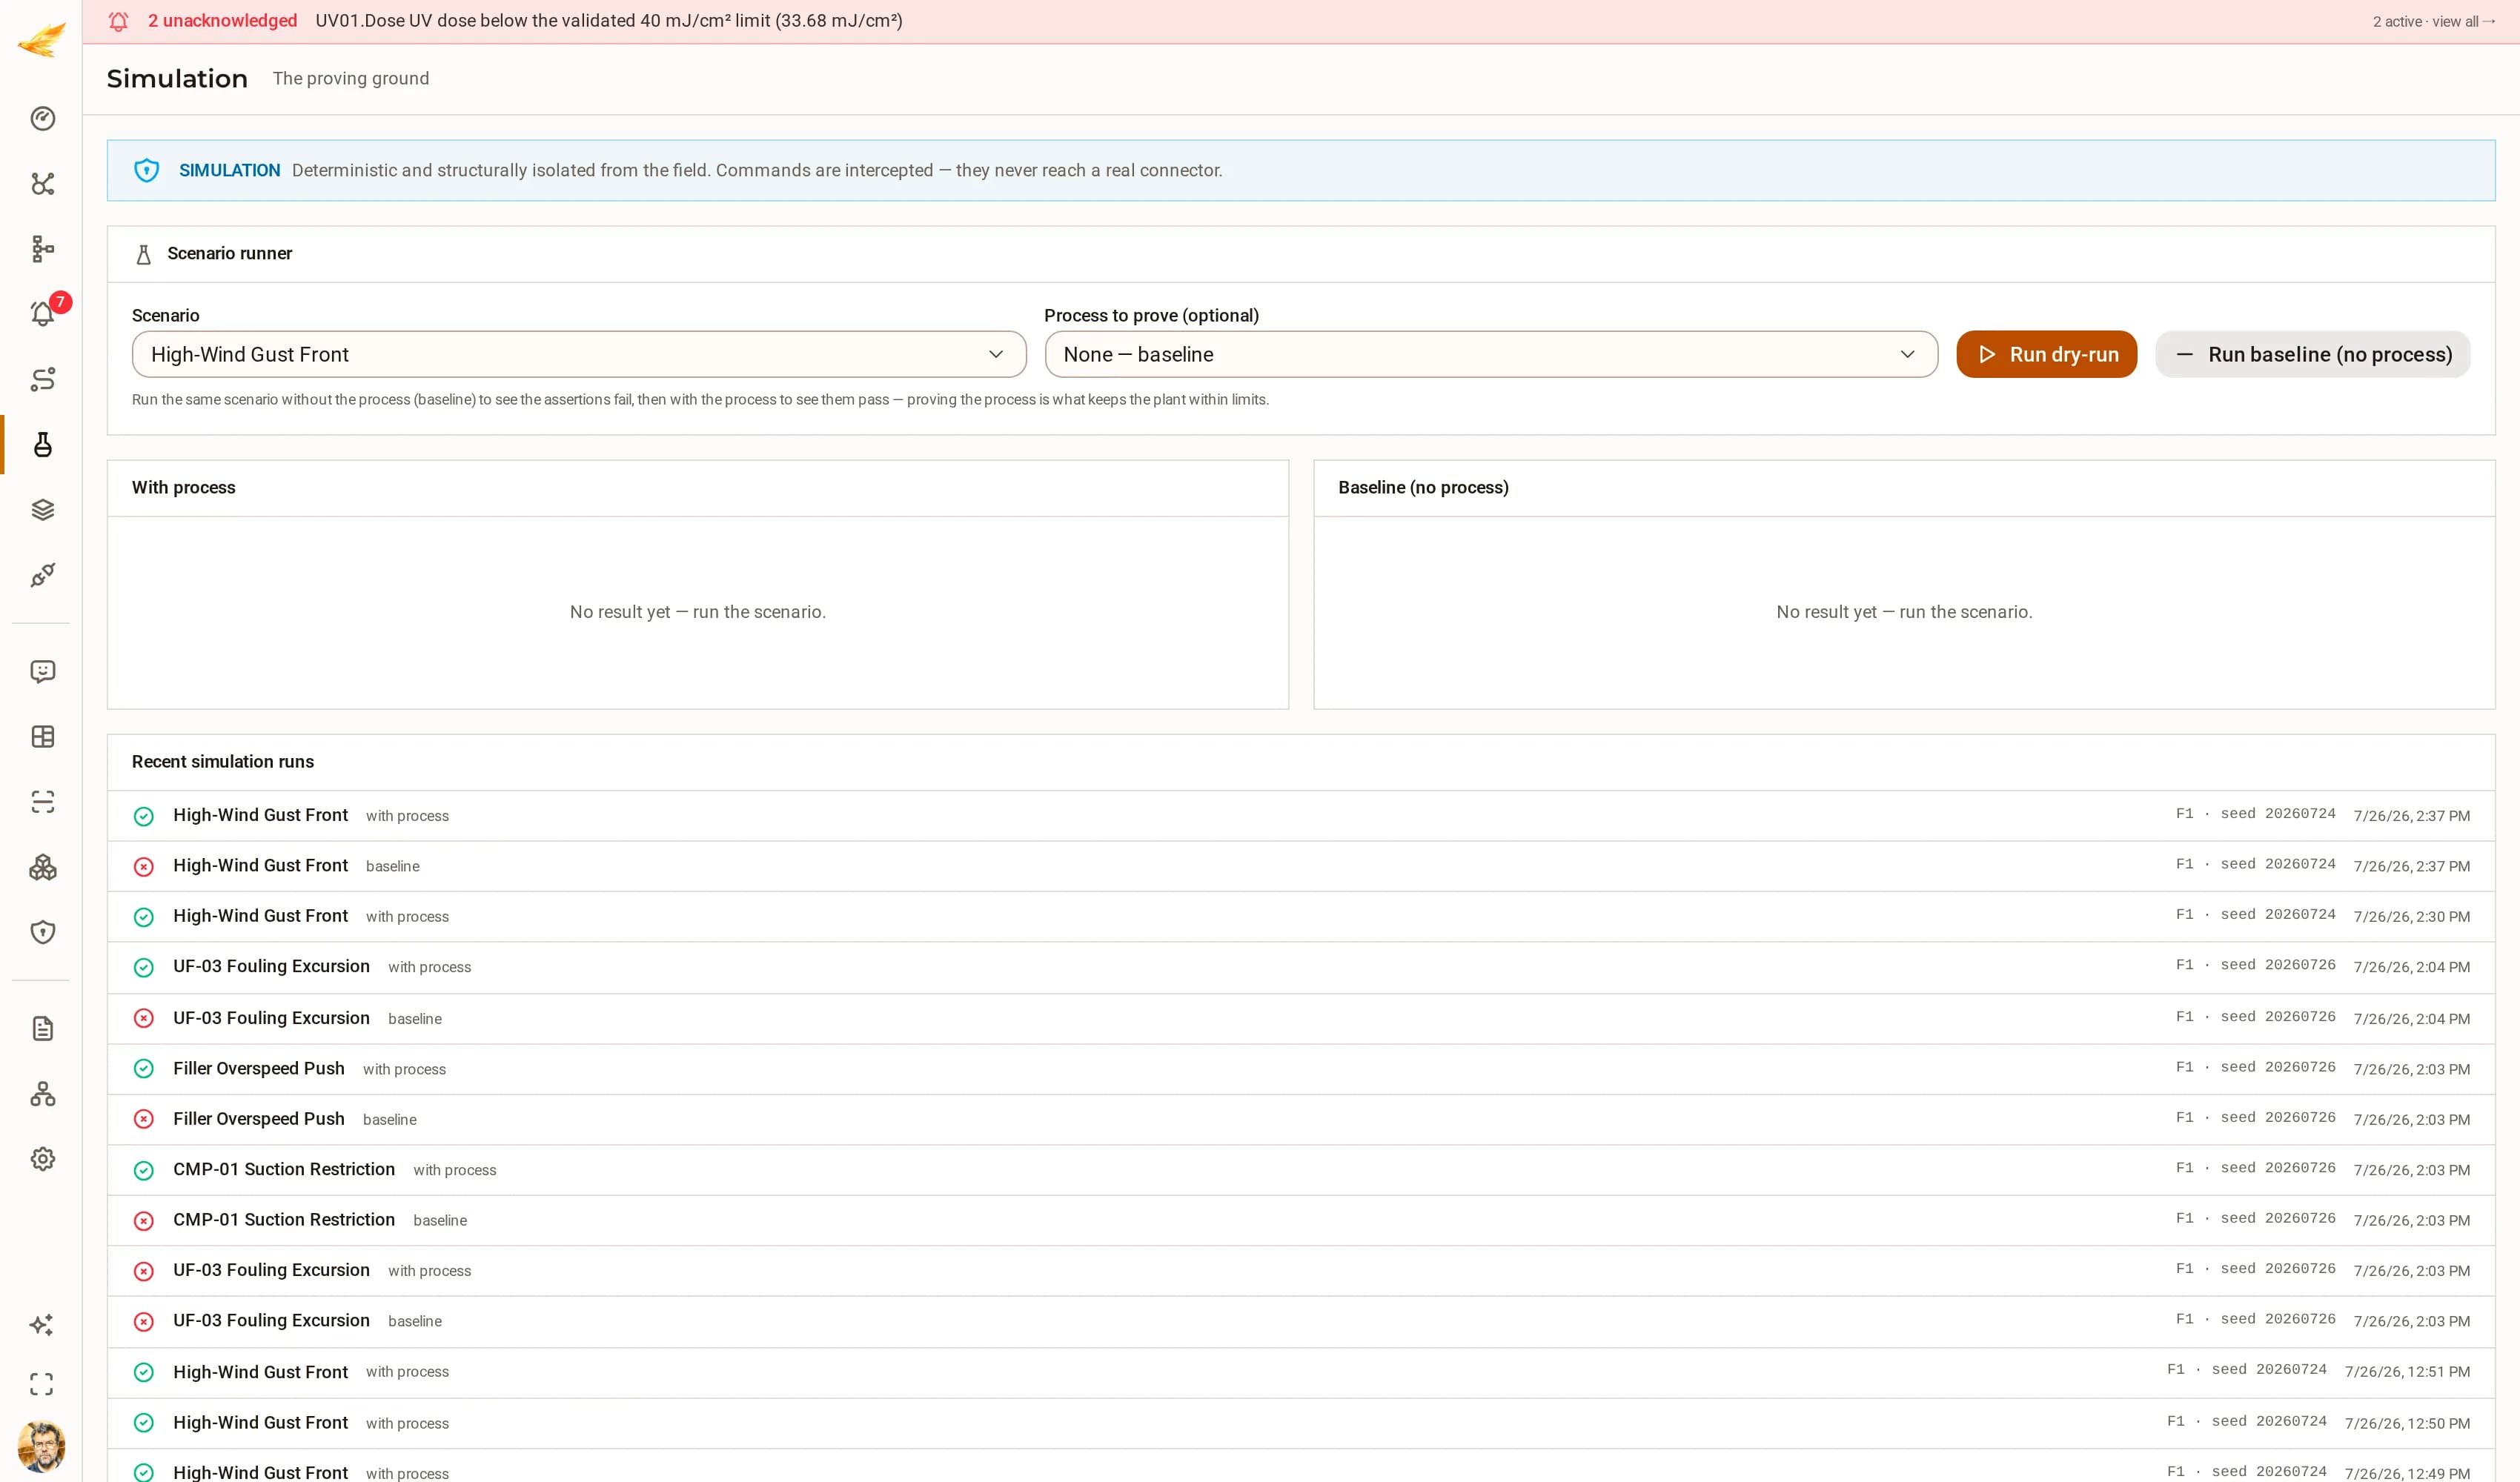
The proof: Filler Overspeed Push
The line is pushed to 100 % of the filler's nameplate rate to chase output; the machine runs beyond its quality knee.
Baseline — without the procedure
- Filler reject rate ≤ 3.5 % — measured 9.40 %
- Filler OEE ≥ 65 % — measured 75.3 %
With the procedure — every assertion holds
- Filler reject rate ≤ 3.5 % — measured 1.90 %
- Filler OEE ≥ 65 % — measured 70.1 %
OEE drops five points and rejects fall by a factor of five. The dry-run shows the operator that trade before the line is touched.
What the control room sees
DjiniousCC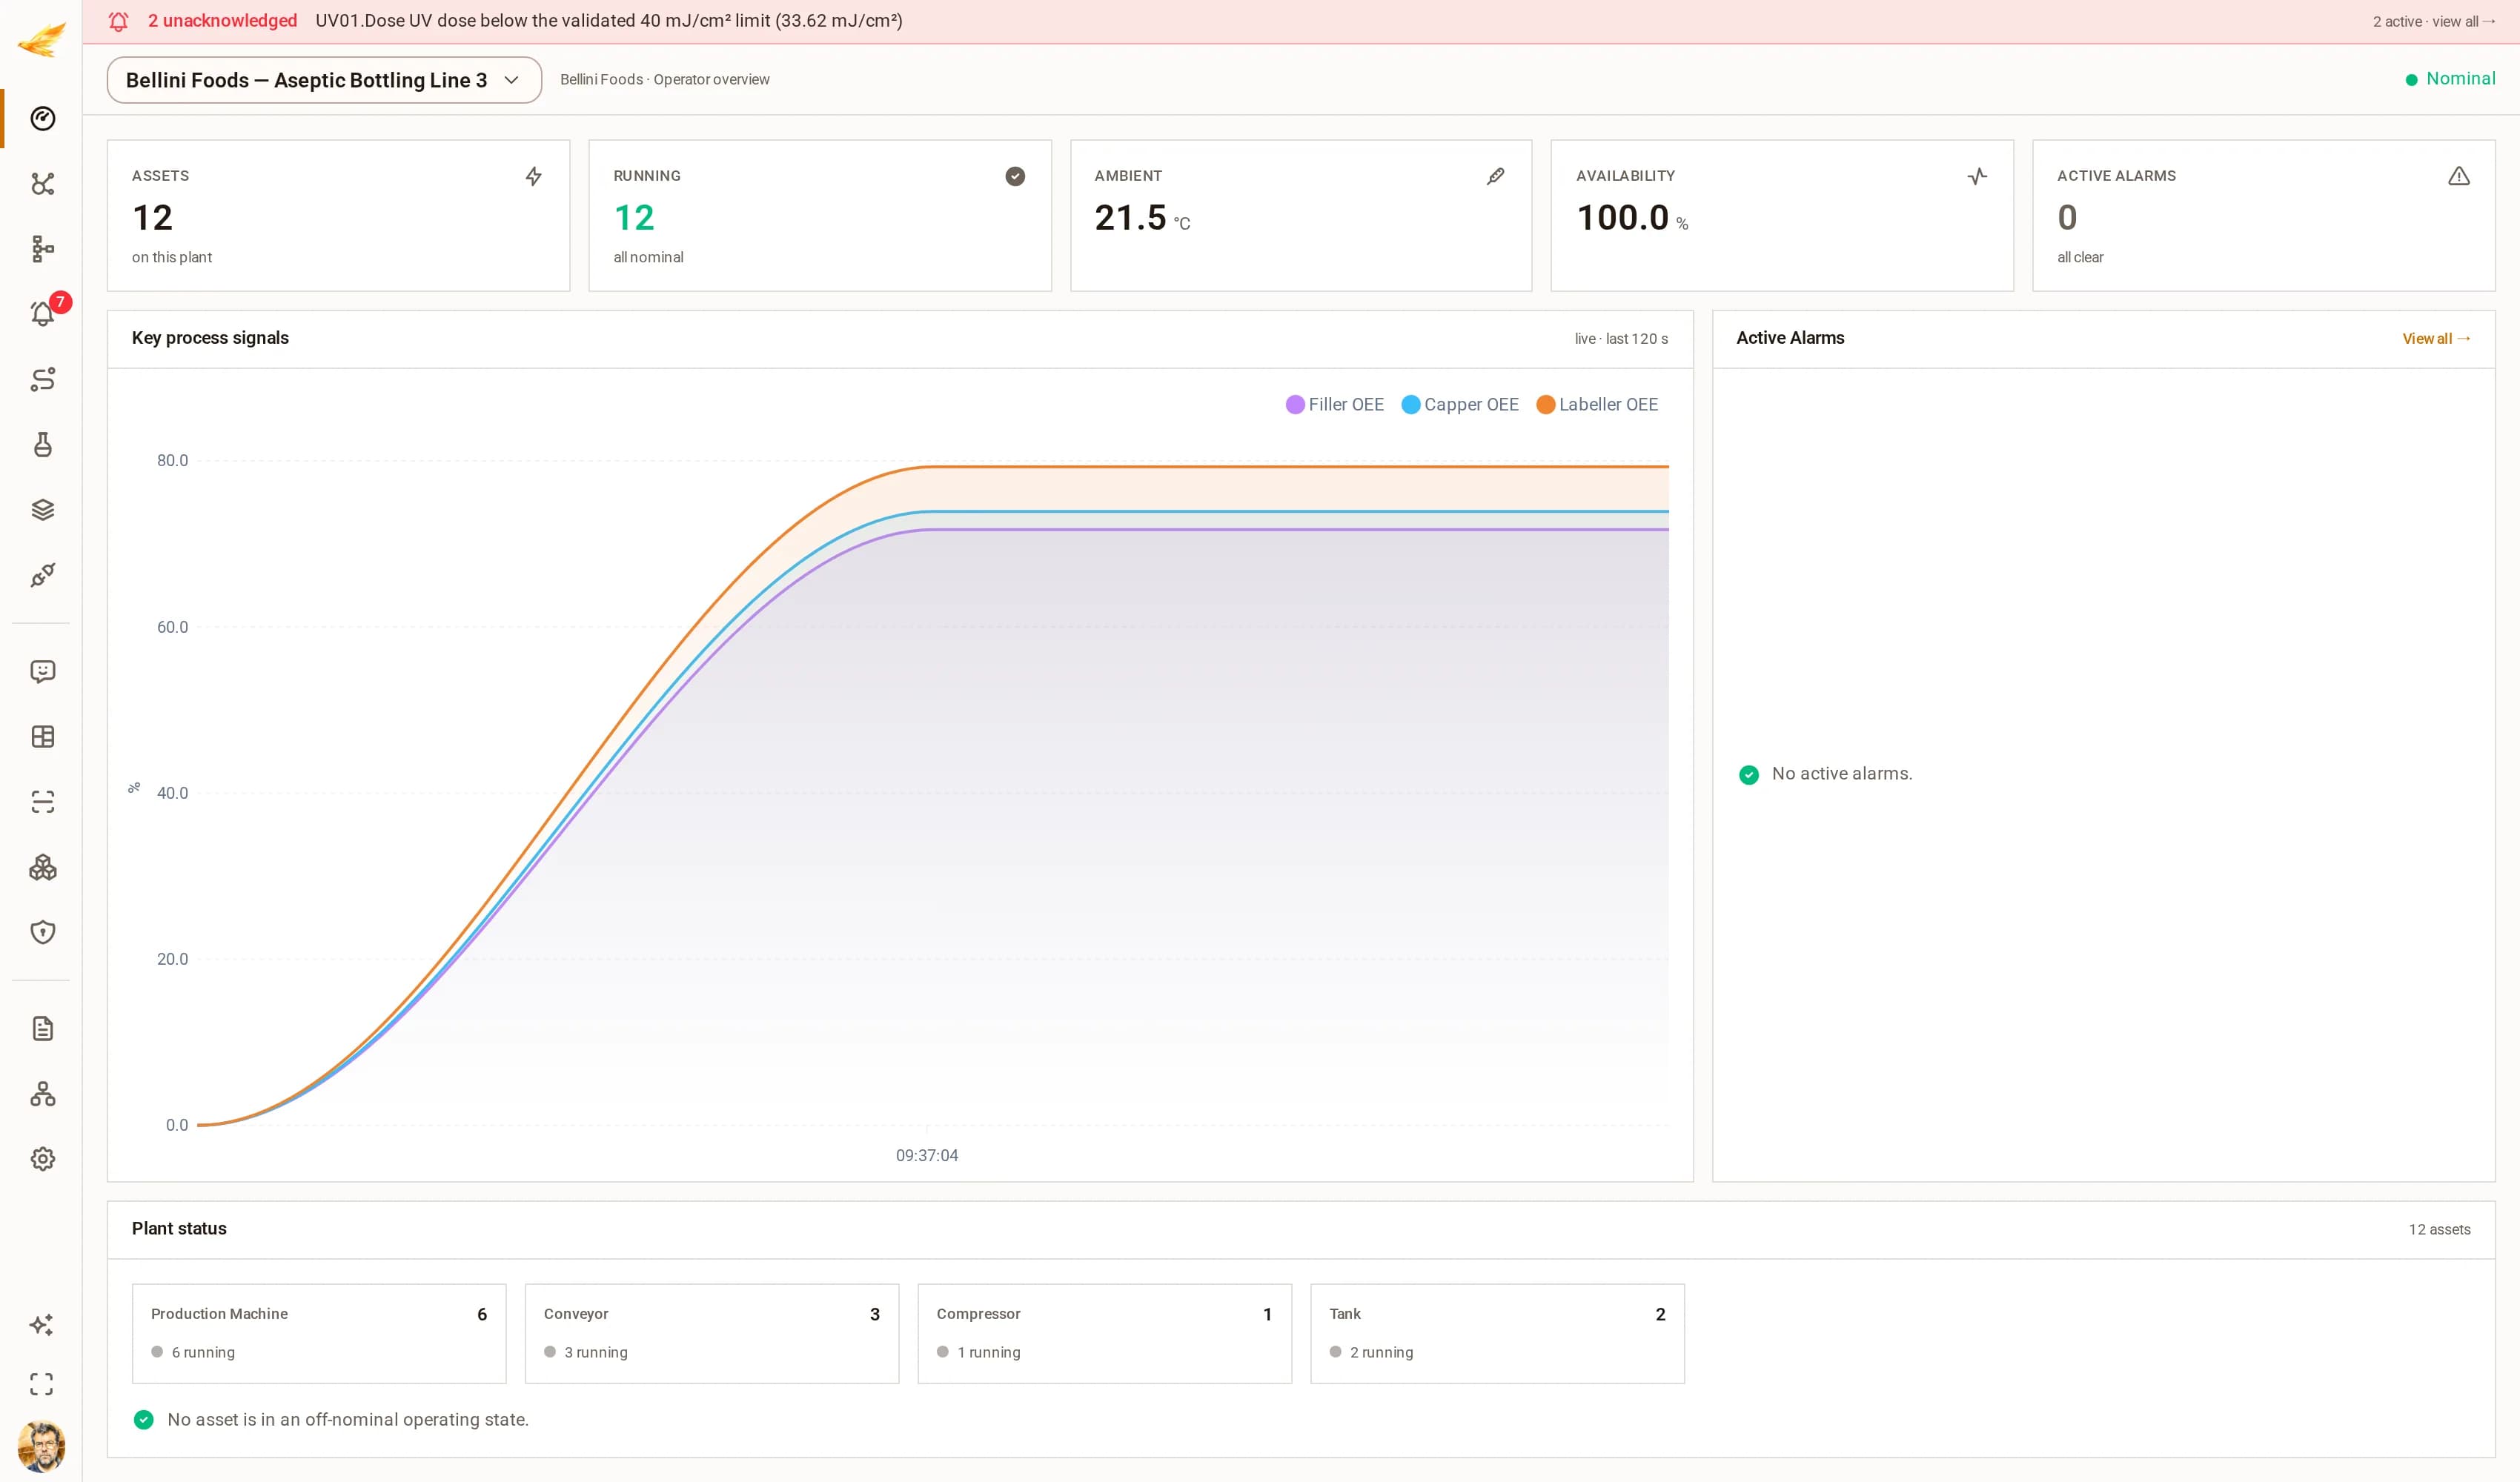 DjiniousCC
Keep exploring
Related use cases
 Industrial roboticsKronos Robotic Work CellA six-axis robotic work cell modelled end to end in ELANG as an audited reference — roughly a thousand lines carrying a functional-safety design to ISO 13849-1 Performance Level d, with every safeguard traced to the hazard it mitigates.
 DjiniousEngineering
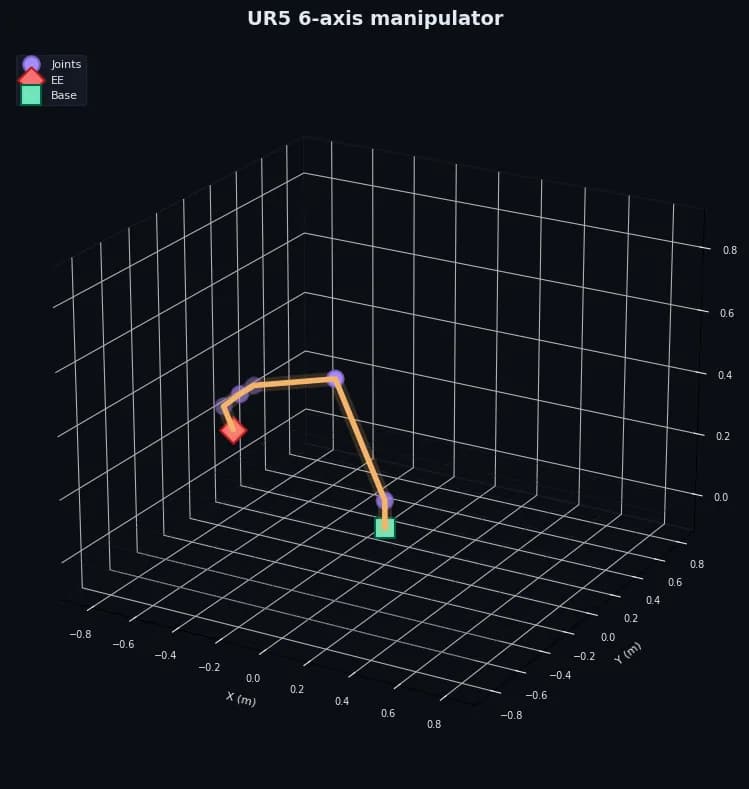 Industrial roboticsUR5 6-axis manipulatorA spatial 6-DoF UR5 arm as one multibody model — closed-form inverse kinematics driving a Cartesian end-effector path through per-joint PD control with gravity feedforward.
 DjiniousLab
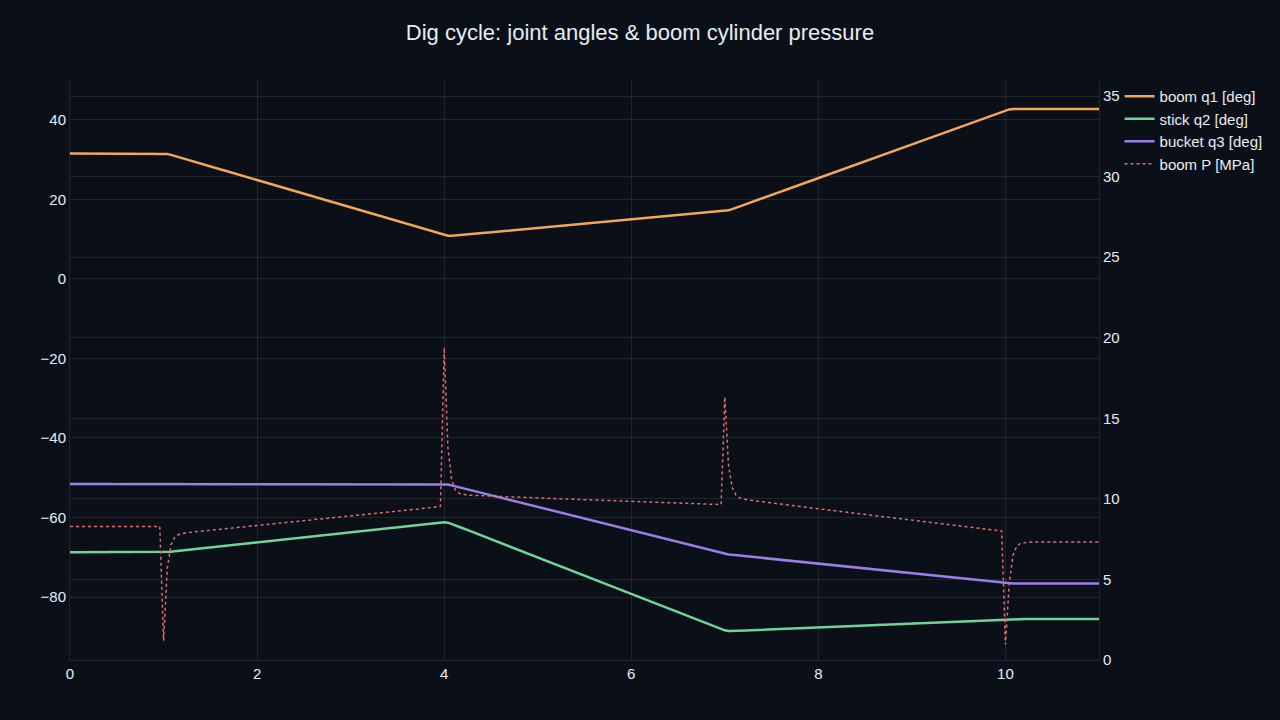 Heavy machineryHydraulic excavatorA 20-tonne excavator as one multi-physics model — a planar boom/stick/bucket linkage driven by hydraulic cylinders off a load-sensing pump, from kinematics and workspace through a coupled dig cycle to breakout force and cycle energy.DjiniousLab